Choosing Channel Magnets for international projects involves more than comparing pull force and price. A magnet that performs well in a warm factory may weaken near a coastal warehouse. A compact channel magnet may also fail when its steel housing, adhesive, or mounting surface changes. Small details matter.
Dr. John M. D. Coey, a respected magnetics researcher, offers a useful principle: “The best magnet is not always the strongest magnet.” That idea guides this practical introduction. Global buyers should examine magnetic grade, channel dimensions, surface coating, operating temperature, and corrosion resistance. They should also request clear drawings, inspection reports, and sample units before placing large orders. A 20-millimeter channel magnet can look perfect on paper, yet fit poorly against a curved steel frame. Testing reveals what specifications sometimes conceal.
The following 10 tips address supplier evaluation, load calculations, packaging, documentation, and quality control. They also consider delivery distances, climate differences, and communication across markets. Reliable suppliers explain tolerances instead of promising perfect results. They identify whether the quoted force applies to clean, flat steel under laboratory conditions. That distinction can prevent expensive mistakes.
Some decisions remain imperfect. Buyers may lack complete field data, especially for new applications. A low-cost sample may create false confidence. We should question convenient answers. Compare several samples, record test conditions, and inspect failures honestly. Strong sourcing depends on evidence, not impressive claims. That is the practical foundation for selecting Channel Magnets with greater confidence worldwide.
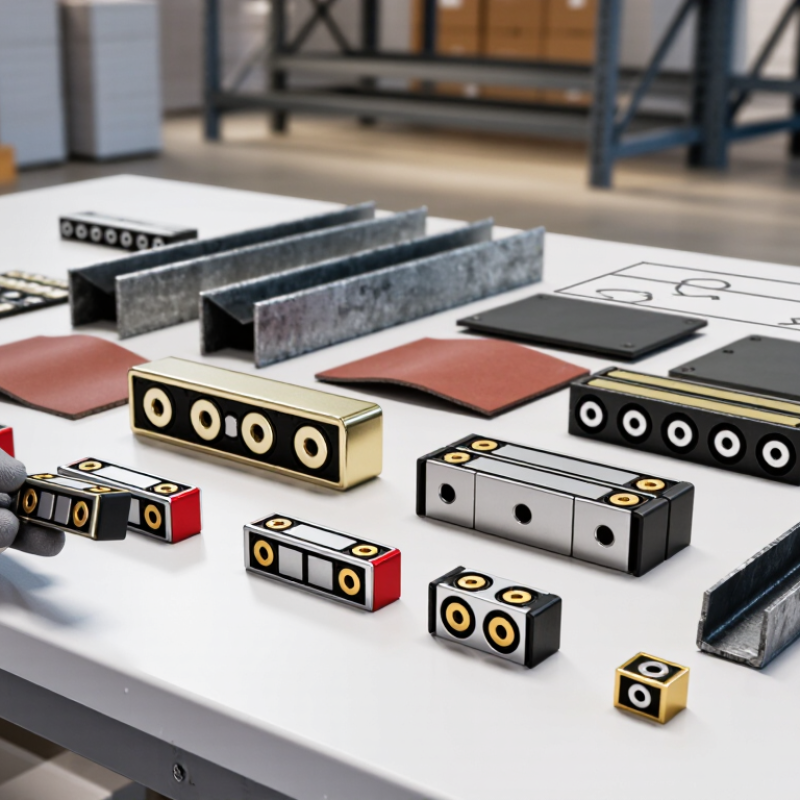
Choosing channel magnets starts with the real job, not the catalog description.
Define the required pull force under actual conditions. A clean steel plate differs from painted, thin, or uneven metal. Add a safety margin for vibration, impact, and movement. Do not treat the published holding value as your working load.
Measure the available space carefully. Record the channel magnet’s length, width, height, and usable contact area. Check nearby edges, screws, cables, and moving parts. Even a few millimeters can affect installation.
Calculate the supported load including the fixture, contents, and possible shock forces. Static weight alone may give false confidence. That mistake is common.
Mounting method matters just as much.
Decide whether the magnet will slide into a channel, sit against a steel surface, or use threaded hardware. Confirm the required access for tools and future replacement.
For overseas projects, share drawings, units, surface materials, and test conditions with the supplier. Clear details reduce costly interpretation errors. I have seen strong magnets fail because the mounting surface was too thin.
A small prototype can reveal this early. Measure twice. Then test the complete assembly in its intended position.
A neat calculation may still miss corrosion, air gaps, or sideways loads. Recheck the design after field testing.
Choosing channel magnets for global applications starts with residual induction, or Br. This value describes the magnetic flux density remaining after magnetization. Typical NdFeB grades provide about 1.0–1.4 T, while ferrite commonly delivers 0.2–0.4 T. These ranges align with engineering data summarized in IEC 60404-8-1 and major magnet material databases.
The difference is visible in practice. A 20-millimeter NdFeB block can produce strong attraction across a small air gap. A ferrite block may need greater thickness or a wider magnetic circuit. That affects channel depth, component weight, and installation clearance. Do not treat Br as holding force. Surface finish, pole geometry, steel thickness, and the air gap can change real performance significantly.
Material choice also depends on supply and operating conditions. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 reported global rare-earth mine production of roughly 390,000 metric tons of rare-earth-oxide equivalent in 2024. This supports careful sourcing for NdFeB projects. Ferrite uses more widely available ceramic raw materials, but its lower Br may increase the magnet volume. Temperature deserves attention. NdFeB can lose performance faster under heat, while ferrite generally tolerates higher temperatures. Still, ferrite is not automatically safer in every design. Test the finished channel assembly, not only the magnet sample. One overlooked air gap can defeat an impressive datasheet value.
For global buyers, temperature grade should match the magnet’s real operating environment. N80°C suits stable indoor assemblies, while H120°C offers more protection near warm motors or sensors. SH150°C, UH180°C, and EH200°C support progressively hotter applications. These ratings describe approximate maximum operating temperatures, not guaranteed performance under every load.
The 2024 U.S. Geological Survey Mineral Commodity Summaries reported global rare-earth mine production of about 350,000 metric tons in 2023. This highlights why material selection and supply continuity deserve equal attention. Higher-temperature grades usually require different alloy designs, which can reduce magnetic strength and increase cost. A strong N-grade magnet may outperform an EH-grade magnet in a cool assembly.
Check the actual coil temperature, housing temperature, duty cycle, and heat-transfer path. Ask suppliers for reversible temperature coefficients, irreversible loss curves, and test conditions. A magnet beside a steel bracket may run hotter than the nearby air suggests. I have seen designs fail because engineers measured ambient temperature only. That was avoidable.
IEC 60404-based measurement practices can improve comparison, but temperature labels are not perfectly uniform across suppliers. Confirm the quoted grade in writing. N80°C may be enough. Sometimes it is not. Leave engineering margin for blocked airflow, repeated starts, and seasonal heat. A laboratory rating can look precise while the field remains less forgiving.
Temperature grades indicate the approximate maximum recommended operating temperature for common sintered neodymium magnet classifications. Actual performance depends on magnetic circuit design, load, coating, working environment, and temperature exposure duration. Select a grade with sufficient thermal margin for the application.
When choosing channel magnets for global buyers, coating verification should be a purchasing requirement, not a catalog detail.
In practical inspections, I check coating thickness, edge coverage, adhesion, and exposed steel around drilled holes. Zinc, nickel, epoxy, and rubber coatings behave differently in humid, salty, or chemically active environments. A clean appearance can mislead.
ISO 9227 salt-spray testing offers comparable corrosion data under controlled laboratory conditions. However, it does not predict exact outdoor service life. That limitation matters.
The NACE IMPACT Study estimated global corrosion costs at 2.5 trillion US dollars annually, equal to about 3.4% of global GDP.
Buyers should request the test method, exposure duration, specimen condition, and failure criteria. A “500-hour result” means little without those details.
Compliance needs separate evidence. Under RoHS, restricted substances include lead, mercury, cadmium, and certain flame retardants. The commonly applied lead limit is 0.1% by weight in homogeneous materials, while cadmium is limited to 0.01%.
REACH screening should include coatings, adhesives, and surface treatments, not only the magnet alloy. Ask for current declarations and laboratory reports linked to the production batch.
Documents may still contain gaps. I have seen certificates that covered the raw material but ignored the final coating. That is an avoidable risk.
Check corrosion resistance again after machining, packaging, and transport exposure.
When choosing channel magnets, treat IEC 60404-8-1 as a material reference, not a complete product guarantee. The standard covers magnetically hard materials, while a finished channel magnet also needs assembly-level tests. Request remanence, coercivity, dimensions, coating thickness, and pull force at a stated air gap. Small details matter. A 1 mm gap can change holding force significantly. ISO 9001 certification shows a supplier has a quality management system, but it does not certify every batch. Check the certificate scope, audit status, inspection records, and corrective-action history. In practice, one missing test report can weaken an otherwise convincing quotation.
Supply risk also deserves direct questions. The International Energy Agency reported that one country produced about 94% of permanent magnets in 2023. This concentration can affect lead times and pricing. Ask for the production location, backup capacity, raw-material origin, and realistic MOQ. A low MOQ may increase unit cost or reduce customization. That trade-off is easy to underestimate. Under Incoterms 2020, FCA can give buyers more control over freight, while DAP places delivery responsibility closer to the seller. Confirm who handles export clearance, insurance, duties, and unloading. Do not assume DDP removes every import obligation. A written quotation should state tolerances, packaging, delivery point, payment terms, and the remedy for nonconforming goods. Reports from the IEA and ISO guidance are useful, but supplier evidence still needs independent checking.
| Tip | Verification Dimension | What to Confirm | Relevant Requirement or Data Point | Recommended Buyer Evidence | Risk-Control Action |
|---|---|---|---|---|---|
| 1 | Define the channel magnet design | Confirm the magnet material, steel channel dimensions, pole arrangement, coating, mounting method, and intended operating environment. | Record length, width, height, hole pattern, magnetic pole orientation, pull-force test method, and allowable dimensional tolerances in the drawing. | Approved 2D drawing, product specification, sample photographs, and a signed technical data sheet. | Freeze the specification before requesting quotations so suppliers quote comparable products. |
| 2 | Check the magnetic material standard | Determine whether the hard magnetic material used in the assembly is covered by the selected material specification. | IEC 60404-8-1 provides specifications for individual magnetically hard materials. It should be applied to the relevant permanent-magnet material, not treated as a blanket certification for the complete channel assembly. | Material grade declaration, lot-specific magnetic test report, and traceability from the material lot to the finished order. | Do not accept “IEC compliant” without identifying the applicable material grade and test basis. |
| 3 | Verify magnetic performance | Compare the required magnetic output with the supplier’s defined test conditions. | Specify the measured property, such as residual induction, coercive force, maximum energy product, surface flux density, or pull force. Pull force depends on air gap, steel thickness, contact area, and test fixture. | Calibration information for the gaussmeter or force gauge, test fixture drawing, sample results, and acceptance limits. | Use the same test method and fixture for supplier samples, pre-shipment inspection, and incoming quality control. |
| 4 | Evaluate corrosion and temperature resistance | Match the magnet coating and assembly materials to humidity, salt exposure, chemicals, and operating temperature. | Review coating type, exposed steel areas, adhesive temperature rating, and the magnet’s reversible and irreversible temperature limits. A coating choice alone does not guarantee corrosion resistance. | Coating specification, environmental test results where required, adhesive technical data, and visual inspection criteria. | Request an application-specific validation test when the product will be used outdoors, in wet areas, or near corrosive chemicals. |
| 5 | Confirm ISO 9001 status | Check whether the manufacturing site has a valid quality management system certificate. | ISO 9001 certification applies to a defined organization, site, and scope. It is evidence of a quality management system and is not, by itself, proof that every magnet meets the required performance. | Current certificate, certificate scope, issuing certification body, validity dates, and manufacturing-site address. | Verify the certificate through the certification body or an accredited certification directory where available. |
| 6 | Assess production capacity and supply continuity | Review normal lead time, monthly capacity, critical raw-material availability, tooling requirements, and backup arrangements. | Ask for a written production schedule covering sample approval, first production, routine production, inspection, and dispatch. Capacity figures should be linked to the specified product and quantity. | Capacity statement, production lead-time history, process flow, contingency plan, and defined escalation contact. | For repeat orders, approve a second source or maintain an agreed safety-stock plan for critical applications. |
| 7 | Clarify MOQ and price breaks | Identify the minimum order quantity for samples, standard production, custom tooling, and each configuration. | MOQ is commercially negotiated and is not fixed by IEC 60404-8-1 or ISO 9001. Request price tiers by quantity, setup charges, packaging charges, and any tooling or sampling fees. | Written quotation showing MOQ, unit price, lead time, payment terms, sample policy, and validity period. | Compare total landed cost at the expected annual volume rather than comparing unit price alone. |
| 8 | Select suitable Incoterms | Define which party controls transport, export clearance, insurance, import clearance, duties, and delivery to the named place. | Incoterms® 2020 should be stated with the named place or port. FCA is commonly used for containerized cargo; FOB is intended for sea or inland-waterway shipments when goods are loaded on board; DAP and DDP allocate different import responsibilities. | Quotation showing the exact rule, named place, shipment mode, cargo insurance responsibility, and customs-document responsibilities. | Do not compare EXW, FOB, CIF, DAP, and DDP prices as if they included the same logistics services. |
| 9 | Control inspection and acceptance | Agree on dimensional, visual, magnetic, coating, packaging, and quantity inspections before production begins. | Define sampling level or inspection quantity, critical dimensions, permissible defects, labeling requirements, and the procedure for handling nonconforming goods. | Inspection plan, approved golden sample, inspection report template, calibration records, and packaging checklist. | Use pre-shipment inspection for new suppliers or high-value orders, and retain batch records for traceability. |
| 10 | Review packaging, documentation, and import readiness | Ensure the shipment is protected from impact, magnetic interference, moisture, and handling damage. | Confirm carton dimensions, pallet requirements, product labels, packing list, commercial invoice, certificate of origin when needed, and any transport or customs documentation applicable to the shipment. | Packaging drawing, carton photos, final packing list, commercial invoice, quality report, and shipment tracking information. | Approve packaging samples for long-distance transport and verify document consistency before dispatch. |
© 1999-2025 The Lincoln Electric Company